Yash Rasayan & Chemicals is a professionally managed manufacturer of pharmaceutical intermediates and specialty chemicals, committed to delivering consistent quality, reliable solutions, and customer-focused service.
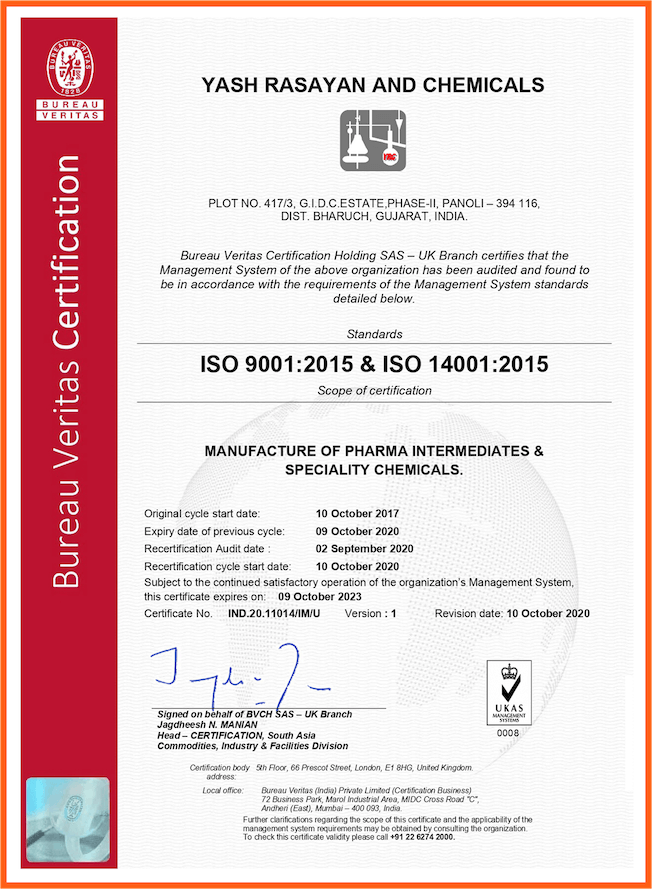
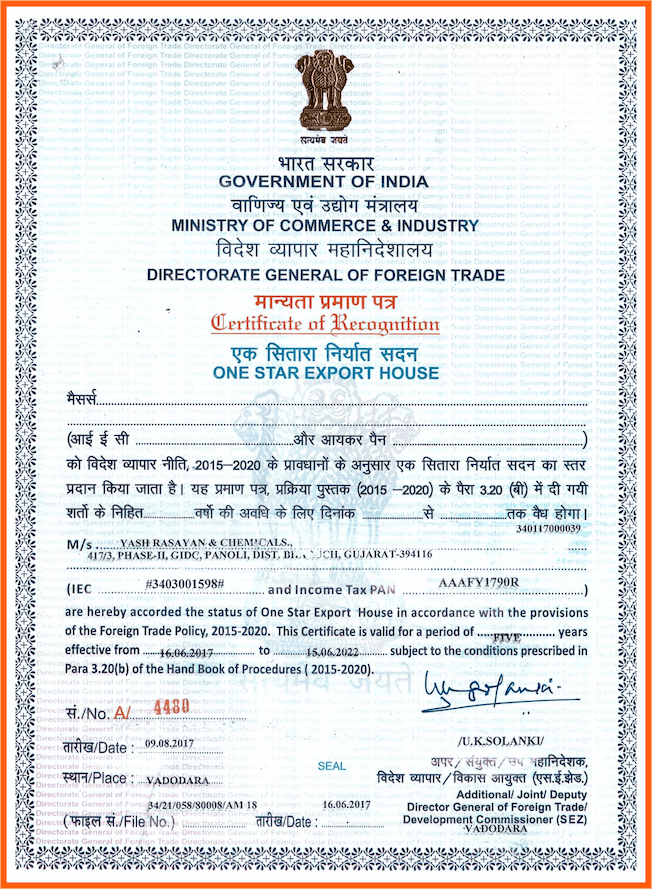
Our manufacturing facility is ISO 9001:2015 and ISO 14001:2015 certified and has been recognized as a One Star Export House by the Government of India. With a strong focus on quality, safety, and operational excellence, we serve customers across domestic and international markets.
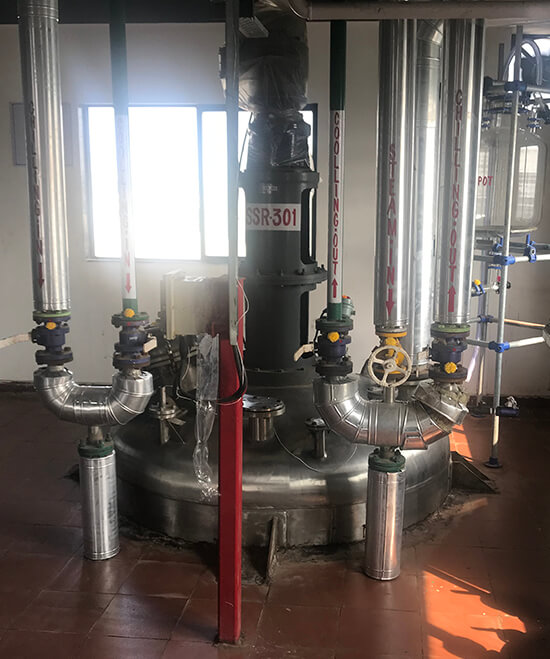
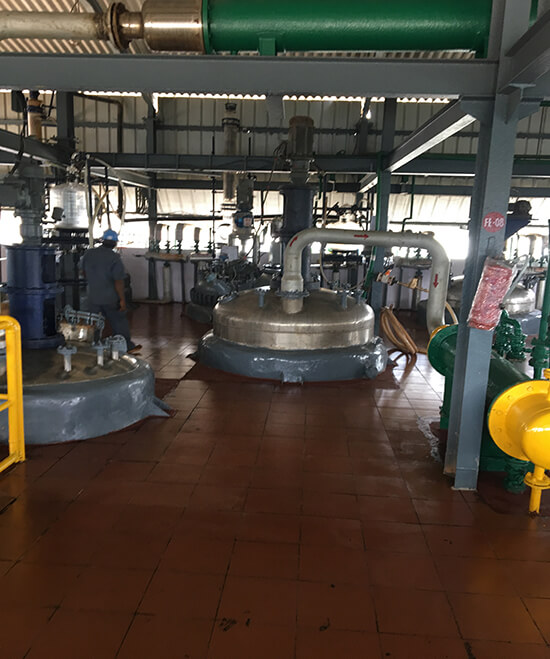
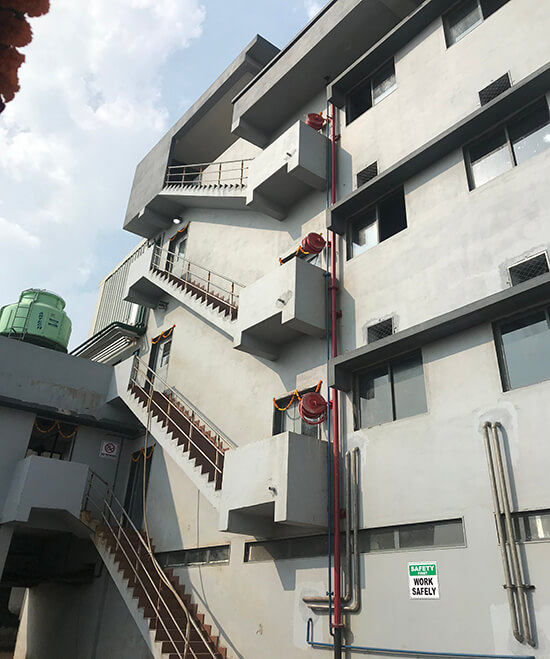
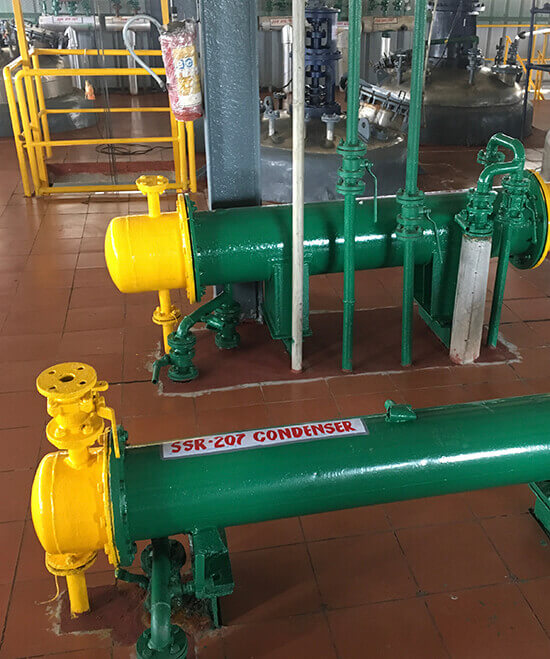
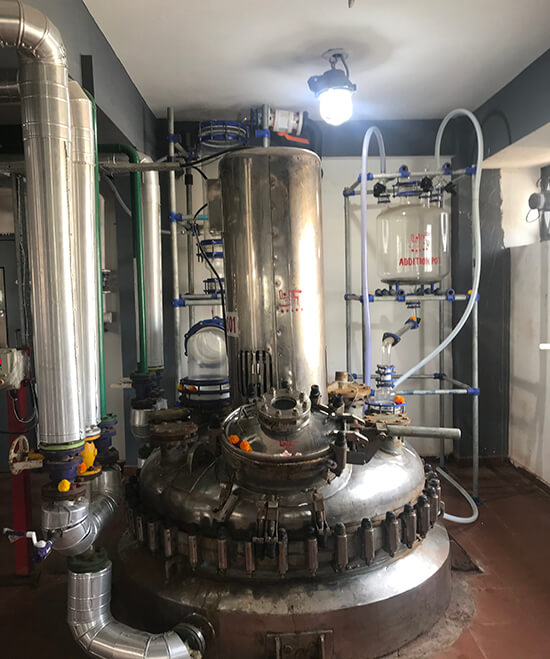
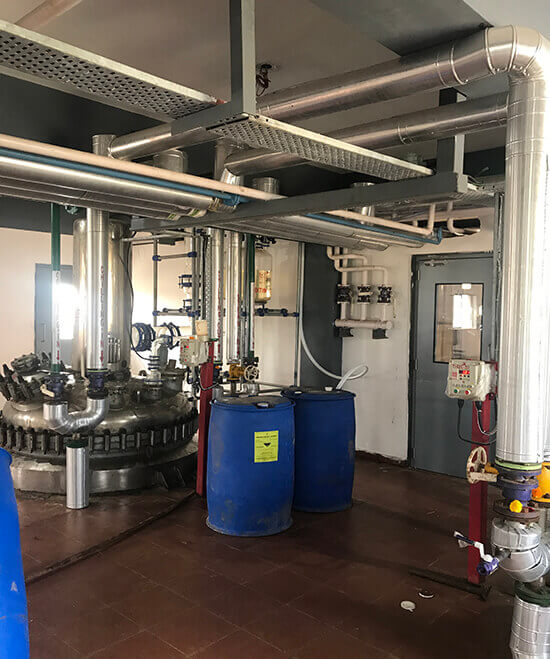
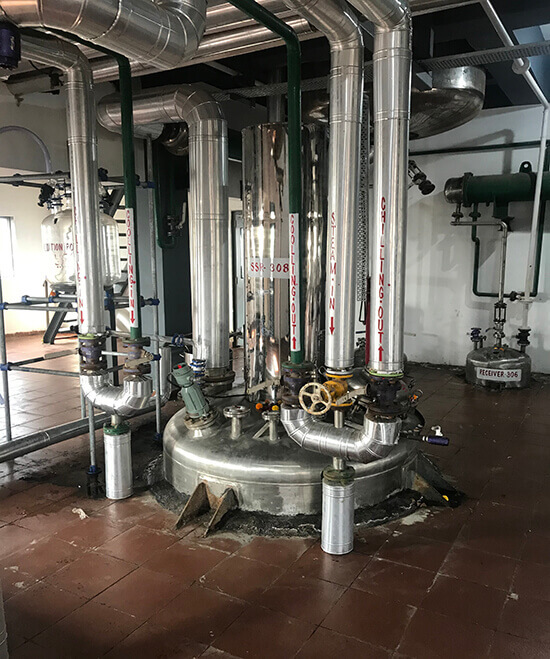
Our facility have Three Block each having its separate production area and Utlity facilities , We have an well equipped Q.C facility and our Quality assurance system Is as per the international standards.
Our manufacturing facility is spread across a total area of approximately 86,000 sq. ft., including 53,600 sq. ft. of built-up area. The facility comprises three dedicated production blocks, each equipped with its own production and utility facilities to support efficient and controlled manufacturing operations.
Our infrastructure is designed to provide a safe, systematic, and reliable environment for the manufacturing of pharmaceutical intermediates and specialty chemicals.
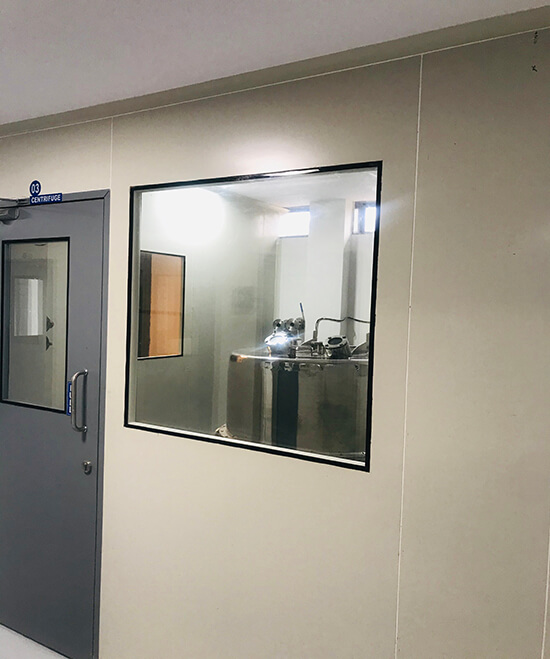
Quality is an integral part of our manufacturing process. We have a well-equipped Quality Control (QC) facility supported by a robust Quality Assurance (QA) system aligned with international quality standards.
Our quality systems focus on maintaining consistency, traceability, process control, and compliance throughout the manufacturing cycle. From raw material evaluation to in-process controls and final product testing, we follow systematic quality procedures to meet customer and regulatory
We provide specialty chemical manufacturing solutions designed to meet the evolving requirements of modern industries. From pharmaceutical intermediates and advanced drug intermediates to specialty chemicals and custom manufacturing, we focus on delivering reliable products backed by strong quality systems, technical expertise, and responsible manufacturing practices.
Through scientific expertise, innovative technologies, stringent quality standards, and a commitment to sustainable practices, we aim to create lasting value for our customers and support the evolving needs of the global pharmaceutical and life sciences industries.
Our mission is to develop, manufacture, and deliver high-quality pharmaceutical intermediates and specialty chemicals that meet the evolving requirements of the pharmaceutical and chemical industries. We are committed to combining scientific expertise, advanced manufacturing capabilities, innovation, and stringent quality standards to consistently deliver reliable and value-driven products.
We strive to build strong and lasting relationships with our customers by understanding their requirements, maintaining consistency in quality, and providing dependable manufacturing solutions. Through continuous improvement, responsible operations, and a strong focus on safety and quality, we aim to create sustainable value for our customers, employees, business partners, and stakeholders.
Our vision is to emerge as a leading pharmaceutical and specialty chemicals company serving global healthcare and industrial needs through innovation, quality, specialization, and responsible growth.
We aspire to strengthen our position in domestic and international markets by continuously enhancing our research capabilities, manufacturing infrastructure, technical expertise, and quality systems. By embracing innovation and adopting modern technologies and efficient manufacturing practices, we aim to develop solutions that meet the changing needs of the global pharmaceutical and life sciences industries.
We envision building an organization recognized for consistent quality, scientific excellence, reliability, customer focus, and responsible manufacturing, while creating long-term value for our customers and business partners. Our commitment is to grow sustainably, expand our global reach, and contribute meaningfully to the advancement of the pharmaceutical and specialty chemicals industry.
We are committed to maintaining high standards of quality, consistency, and operational excellence across our products and processes.
We encourage scientific thinking, continuous improvement, and innovative approaches to develop effective solutions for evolving industry requirements.
We conduct our business with integrity, transparency, accountability, and responsibility, while maintaining respect for people, safety, and the environment.
We build lasting relationships by understanding customer requirements and delivering reliable products, consistent quality, and responsive service.
The focus is to become the largest manufacturer for Pharmaceuticals & Speciality Chemicals, We are looking to enhance our Products, Infrastructure & New developments and are moving ahead with a growth mindset.
Planning our Business roadmap keeping our theme of Growth. To create the bright future of the company “TOGETHER WE GROW”.
Join us to experience cutting-edge Chemical solutions that drive innovation, lasting success.
Copyright © 2026 Yash Rasayan. All rights reserved.
No WhatsApp Number Found!
WhatsApp us